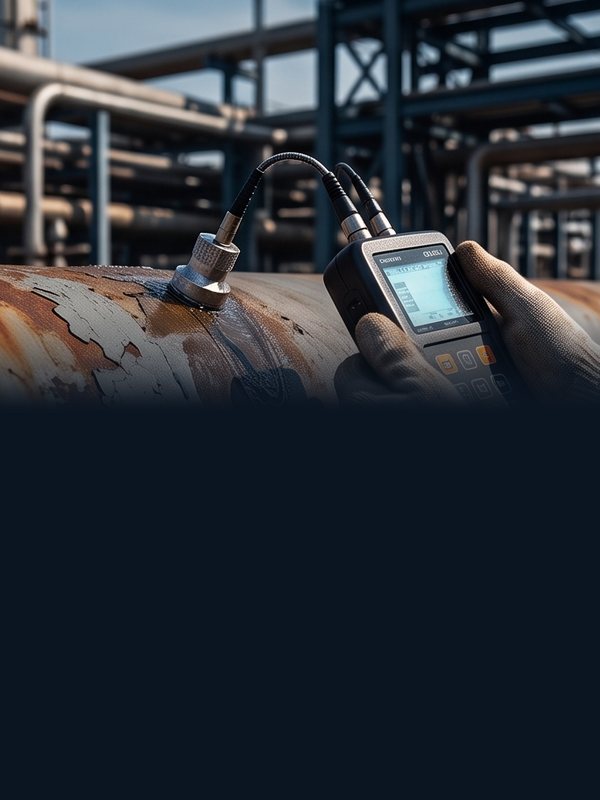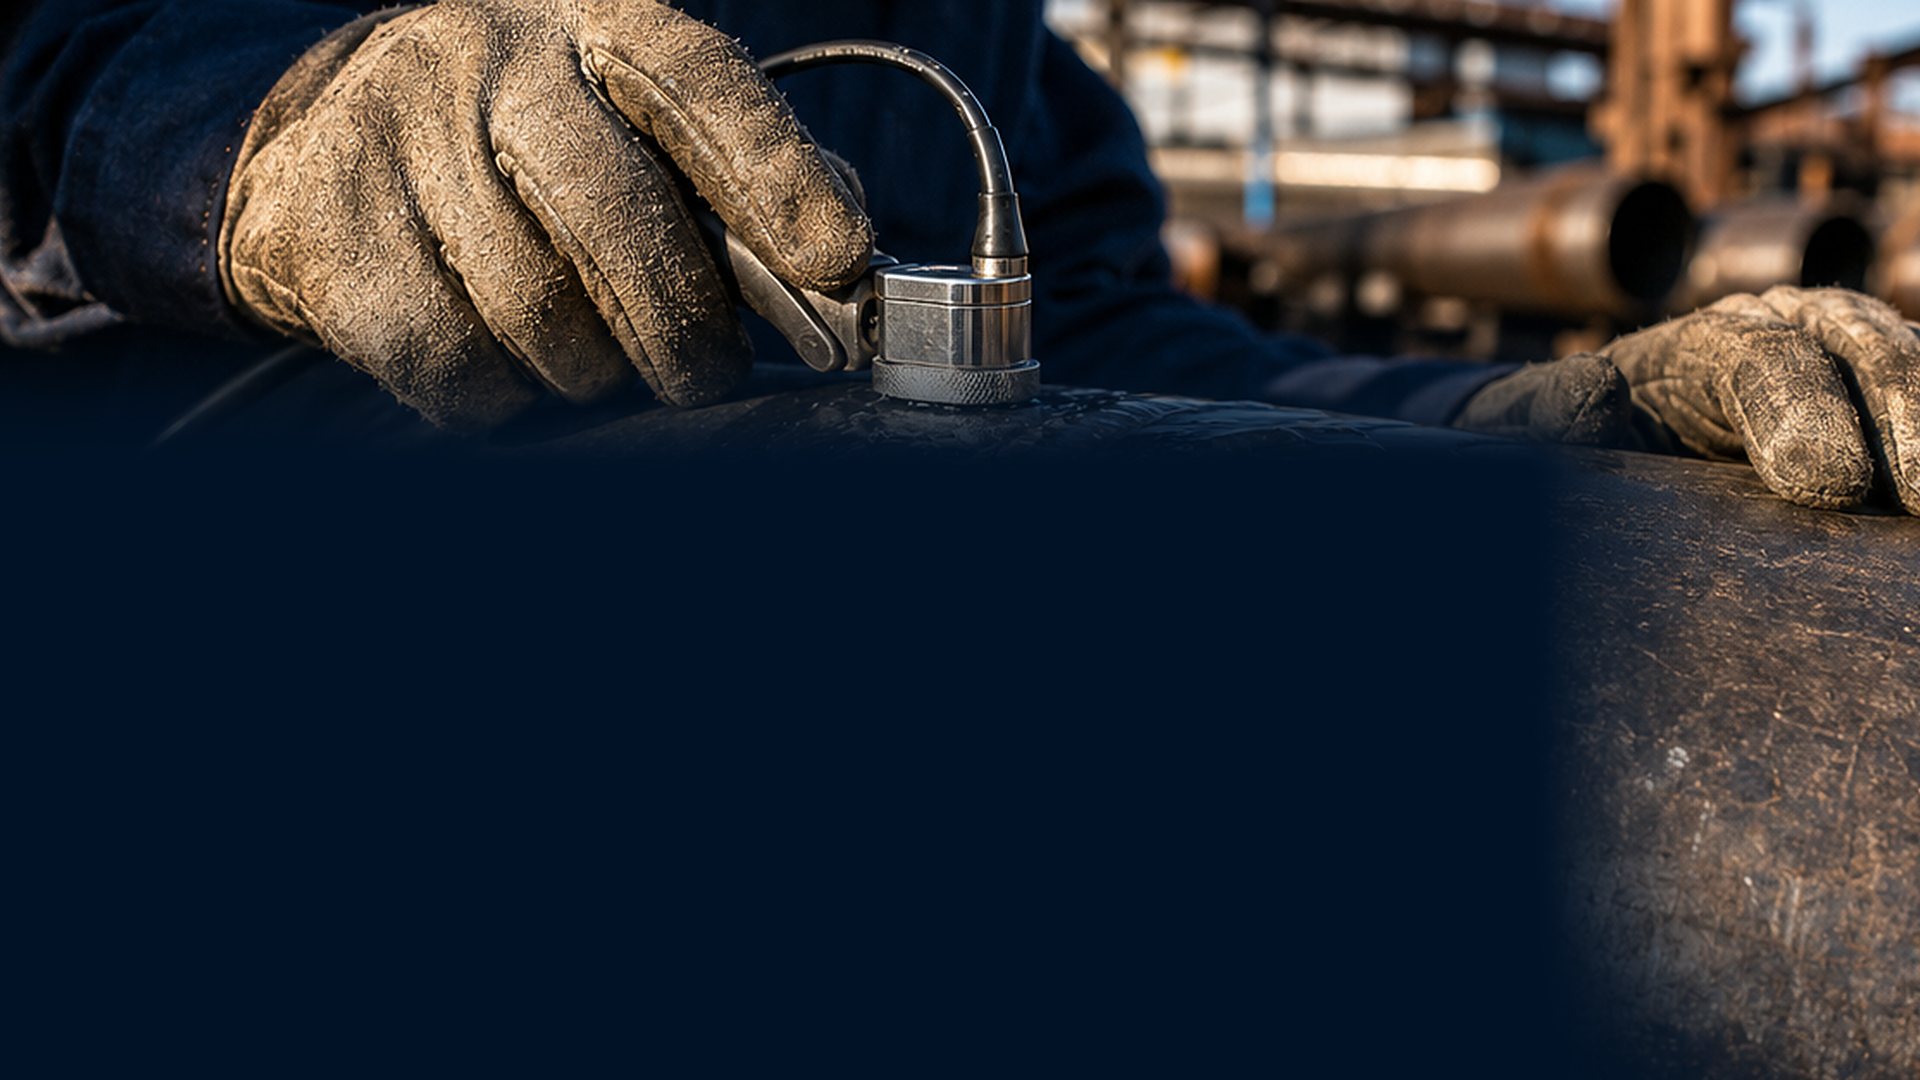
Ultrasonic testing on a weld reports the flaws that reflect sound back to the probe, and stays quiet about the ones that do not.
Adapted for the web from the original post of 10 September 2026.
Ultrasonic testing on a weld reports the flaws that reflect sound back to the probe, and stays quiet about the ones that do not.
UT is strong on planar flaws facing the beam — lack of fusion, cracks, laminations.
A tight crack lying along the beam, or fine surface-breaking porosity, can pass through it.
The method answers the question it was set up to answer, and no more.
The weld passed UT and the weld is sound are not the same sentence. The gap between them is whatever UT was blind to.
When a weld on your plant clears UT, does the inspection plan also cover what UT cannot see, or does it stop at the one method?
Fixed-scope and fixed-price, quoted in writing before work begins.
Choosing the right combination of methods for a given weld and a given defect concern is part of what OMNIX does. If weld inspection is single-method by default, the coverage may be narrower than the report reads. OMNIX's NDT work covers ultrasonic wall-thickness testing and corrosion mapping, magnetic particle crack detection on welds and structures, and dye penetrant surface inspection for non-ferrous components, with every finding located and photographed. Which Indian Standards apply depends on your equipment and its duty.
The weld passed UT and the weld is sound are not the same sentence.
Short notes on machines, steam, fire systems and NDT — each first posted on LinkedIn.
Tell us your unit name, location and the equipment or premises concerned. A thirty-minute walkthrough at your plant — travel included within Visakhapatnam city limits, quoted in advance for outstation sites.